Top 10 Explosion-Proof Robots for Global Buyers
Choosing the right Explosion-Proof Robot requires more than comparing cameras, payloads, and battery life. Global buyers need equipment that can operate reliably where flammable gases, vapors, dust, or fibers may create serious risks. These environments include refineries, chemical plants, underground mines, fuel storage areas, and selected manufacturing sites. Small details matter.
This guide reviews ten leading robot options for international purchasing teams. It considers hazardous-area certification, mobility, communication range, sensor performance, thermal imaging, remote operation, maintenance access, and total ownership cost. A robot may carry advanced sensors, yet remain unsuitable if its certification does not match the facility’s zone classification. Buyers should verify documentation, local approvals, operating temperature limits, ingress protection, and replacement-part availability before signing a contract.
No ranking is perfect. Product specifications can change, regional certifications may differ, and field performance depends on training, floor conditions, network coverage, and maintenance discipline. That point deserves attention. A tracked robot that crosses wet concrete may struggle on loose gravel or steep metal stairs. Likewise, a long-range wireless system may weaken inside reinforced structures. Our comparison therefore combines manufacturer data, practical deployment considerations, and risk-focused purchasing criteria. It does not replace a site assessment or qualified safety review. Instead, it provides a clearer starting point for buyers who need dependable inspection, monitoring, and emergency-support capabilities without compromising regulatory compliance or worker protection. The best choice is rarely the most expensive model. Fit is everything.
Explosion-Proof Robot Fundamentals and Hazardous-Area Standards
Explosion-Proof Robots for Global Buyers
Explosion-proof robots are built to operate where flammable gases, vapors, or dust may ignite. Their protection can include flameproof enclosures, intrinsic safety, purging, or restricted-energy circuits. Each method controls ignition differently. A sealed housing alone is not enough. Motors, batteries, sensors, connectors, and cable entries can all create heat or sparks. Temperature classification matters. So does the equipment protection level.
Hazardous-area selection begins with the site classification. Gas zones commonly include Zone 0, Zone 1, and Zone 2. Dust zones include Zone 20, Zone 21, and Zone 22. Engineers must also check gas groups, dust groups, ambient temperature, and required ingress protection. IEC 60079 standards provide a major technical foundation, while IECEx supports international certification. ATEX requirements apply within relevant European markets, and NEC and NFPA rules guide many installations in the United States. Local approval still matters.
Real facilities are rarely clean.
Oil residue, vibration, and damaged seals can reduce protection. A robot certified for one zone may not suit another zone or process. Buyers should review the complete certificate, not only the robot body. Battery modules and replacement parts need equal attention. In practice, rushed procurement often overlooks maintenance access. That weakness deserves honest review before deployment. Certified inspection, documented training, and scheduled testing help keep the protection system reliable.
Key Features for Evaluating Explosion-Proof Robots
Top 10 Explosion-Proof Robots for Global Buyers
Key Features for Evaluating Explosion-Proof Robots
Evaluating an explosion-proof robot starts with certification, not marketing language. IECEx or ATEX documents should identify the exact model, protection method, hazardous-zone rating, gas or dust group, and temperature class. Zone 0, 1, and 2 requirements differ. So do Zones 20, 21, and 22. An IP66 enclosure resists dust and water, but it does not replace hazardous-area certification. This distinction is often missed.
Match the robot to the task. Check payload at full reach, stopping accuracy, operating temperature, battery chemistry, and cleaning method. A compact crawler may inspect a narrow pipe. A mobile unit needs stable traction on grated floors. Sensors should detect gas, heat, obstacles, and communication loss. Remote operation needs encrypted links, event logs, and a safe failure mode. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in World Robotics 2024. Grand View Research estimated the industrial robotics market at roughly 19 billion dollars in 2023. Growth does not guarantee suitability.
Review maintenance evidence before purchase. Ask for test reports, certificate schedules, spare-part lead times, firmware controls, and operator training records. The IECEx online certificate system supports document verification during audits. Battery charging may need to occur outside hazardous areas. A glossy demonstration proves little. Field trials should measure heat buildup, radio dropouts, wheel slip, and fault recovery. No checklist is perfect. Claims without independent test evidence deserve doubt.
Top 10 Explosion-Proof Robots for Global Buyers
Top 10 Explosion-Proof Robots for Global Buyers
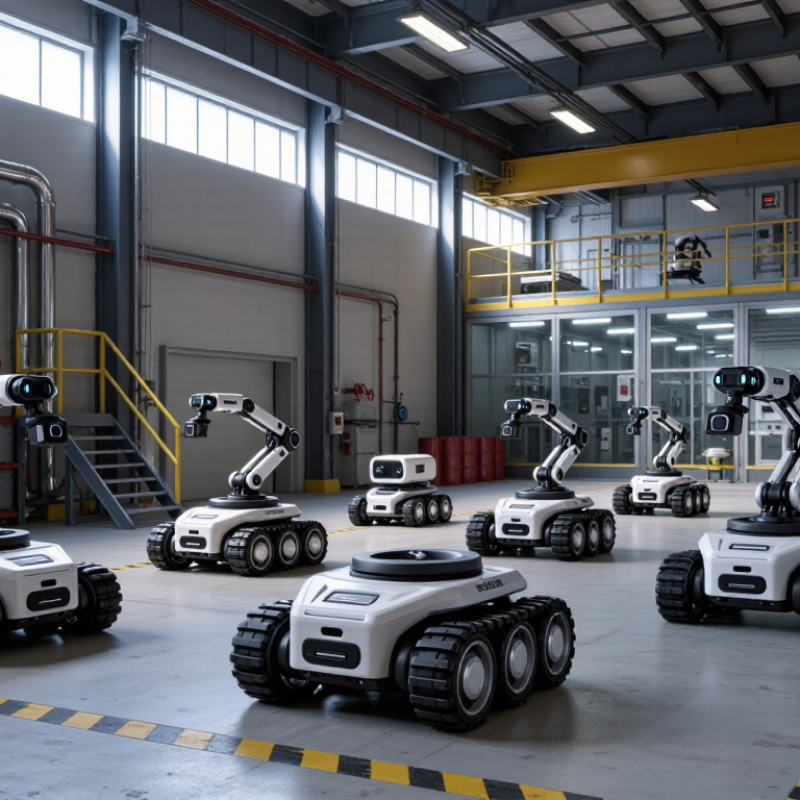
The top ten explosion-proof robots serve different industrial inspection needs. They include mobile patrol robots, tracked inspection robots, pipeline crawlers, tank-inspection units, and confined-space robots. Other useful categories include gas-detection robots, thermal-imaging robots, wheeled mapping robots, robotic arms, and aerial systems approved for hazardous zones. Each option should match the site, not merely the sales description. A refinery may need continuous gas sensing, while a grain facility may prioritize dust protection and low-temperature operation.
Safety evidence matters more than impressive movement. Buyers should check applicable IECEx, ATEX, or local certifications before comparing cameras or battery size. Confirm the certified zone, gas or dust group, temperature class, ingress rating, and charging procedure. Ask for test documents, maintenance intervals, and remote-control operating limits. Field experience also shows that narrow stairways, wet floors, radio shadows, and poor lighting can reduce performance quickly. Small details matter.
Reliable models usually provide sealed housings, emergency stop functions, obstacle detection, and clear video transmission. Some carry methane, volatile-compound, oxygen, or particulate sensors. Sensor accuracy depends on calibration and environmental conditions. No ranking is perfect. A robot that performs well in a dry plant may struggle inside a humid tank. Battery endurance may also disappoint during cold-weather patrols. Global buyers should request site trials, operator training, spare-part plans, and local technical support before placing an order.
Industry Applications and International Compliance Requirements
Top 10 Explosion-Proof Robots for Global Buyers
For global buyers, the best explosion-proof robot is not always the fastest model. It must match the hazardous area, process duty, and local approval system. Useful options include inspection crawlers, remote visual units, gas-monitoring robots, tracked utility robots, robotic arms, pipeline crawlers, tank-inspection units, firefighting platforms, warehouse vehicles, and mining robots.
These machines support petrochemical plants, fuel terminals, chemical facilities, grain processing sites, underground mines, and paint operations. Each application creates different risks. A tank robot may need sealed cameras and corrosion-resistant housing. A mining robot may require strong traction, low-light imaging, and reliable communication through concrete or rock. A gas-monitoring unit should identify sensor range, response time, calibration records, and alarm behavior.
Compliance requires careful verification. Buyers should check equipment protection levels, temperature class, ingress protection, and permitted gas or dust groups. Common international references include IECEx and regional systems such as ATEX. Some markets also request local certification, import documents, quality records, and installation assessments. Certification must cover the complete robot, not only one electrical component. Testing matters.
A practical review should examine wiring, battery design, charging procedures, emergency shutdown, software updates, and maintenance access. Suppliers should provide certificates, test reports, manuals, and traceable serial numbers. Details matter. A recurring mistake is accepting a certificate without checking its exact model and hazardous-zone scope. No checklist is perfect. Field conditions, operator training, and future repairs still deserve honest review.
Top 10 Explosion-Proof Robots for Global Buyers
Typical payload capacity by industry application and international compliance focus
The chart compares representative payload capacities commonly specified for explosion-proof robotic systems across major industrial applications. Hazardous-area deployments typically require certification aligned with ATEX or IECEx requirements, together with suitable IP protection, temperature classification, and gas or dust group assessment. Actual performance depends on the robot configuration, operating zone, payload definition, and certification scope.
Selection Criteria, Costs, Maintenance, and Supplier Support
Top 10 Explosion-Proof Robots for Global Buyers
Selecting an explosion-proof robot begins with the worksite, not the product brochure. Identify gas, vapor, dust, temperature, and humidity risks first. Verify certification for the intended hazardous area and local authority requirements. A robot designed for chemical inspection may not suit grain dust or fuel storage. Check payload, reach, traction, camera quality, and remote-control stability. Small details matter. A weak radio link can stop an inspection beside a steel tank.
Cost planning should include more than the purchase price. Add transport, installation, operator training, certification review, spare batteries, software, and annual testing. A lower-priced unit can become expensive when replacement parts require international shipping. Request a clear warranty period and written service response times. Suppliers should provide manuals, repair procedures, diagnostic logs, and practical training. Ask whether technicians can support different time zones. Vague answers deserve caution.
Maintenance should fit the site routine. Inspect seals, wheels, connectors, lights, sensors, and battery housings after each operation. Keep a simple service record with dates and fault descriptions. Dust buildup is easy to underestimate. It can affect cooling and sensor accuracy. Supplier support also needs testing before purchase. Arrange a sample demonstration, preferably under similar lighting, flooring, and communication conditions. The “best” robot may still fail when turning on wet grating. Selection is rarely perfect, so record assumptions and review them after the first month of use.